Glossary · Manufacturing
Lean and Toyota Production System
136 terms in the Manufacturing glossary, each with its one-line definition.
136 terms, A to Z
- 5 Whys Problem solving method that asks why a problem happened, then why again about each answer, until it reaches a root cause the team can fix.
- 5S Workplace organization method of sort, set in order, shine, standardize and sustain that gives everything a place and makes problems easy to see.
- A3 Report One page document on A3 paper that tells the full story of a problem, its root cause, countermeasures and follow up, used for coaching and review.
- Abnormality Management Practice of defining normal conditions clearly so any deviation stands out at once and triggers a fast, defined response and escalation.
- Andon Signal of lights, sounds or a board that shows line status and lets an operator call for help the moment something goes wrong.
- Batch and Queue Traditional way of producing in large lots that then wait in piles before the next step, creating inventory, delay and hidden defects.
- Bowling Chart Table tracking a few key metrics month by month against target, with each cell colored green when met and red when missed.
- Built-in Quality Principle that each operator and process makes sure work is right before passing it on, instead of relying on inspection at the end of the line.
- Catchball Back and forth dialog that passes goals and plans between levels of a company until each level agrees on the part it will own.
- Cellular Manufacturing Grouping all the machines needed for a family of similar products into a compact cell, often U shaped, so parts move straight from step to step.
- Chaku-Chaku Cell where machines unload parts automatically so the operator only walks the loop loading each part into the next machine.
- Chief Engineer Single leader who owns a whole product from concept and customer value to cost, launch and profit, leading through expertise more than authority.
- Coaching Kata Daily coaching routine of five standard questions that a coach uses to teach the improvement kata and build the learner's problem solving skill.
- Constant Work in Process CONWIP Pull control method that caps the total work allowed inside a line and releases a new job only when a finished one leaves.
- Continuous Flow Making and moving products one at a time, or in tiny consistent batches, through each step with no waiting piles in between.
- Cost Deployment World Class Manufacturing method that converts every plant loss into money, traces it to its cause and ranks improvement projects by payoff.
- Countermeasure Action taken against the root cause of a problem, treated as the best current attempt that must be checked and may later be improved.
- Current State Map First value stream map, drawn by walking the process, showing how material and information really flow today with times and inventory.
- Cycle Time Time to finish one unit at a machine or station, measured from the start of one unit to the start of the next, and compared with takt time.
- Daily Management Shift routine of visual boards, short tiered meetings, leader checks and action follow up that keeps work on plan and surfaces problems fast.
- Eighth Waste Waste of not using people's skills, ideas and creativity, added by Western practitioners to Ohno's original seven wastes.
- Electronic Kanban e-kanban Kanban whose replenishment signal is sent electronically by barcode or RFID scan instead of a physical card, common for distant suppliers.
- Every Part Every Interval EPEI How often a process can cycle through every product variant given the time lost to changeovers, so a shorter interval means smaller batches.
- External Setup Changeover work done while the machine is still running the previous job, such as staging the next die, which shortens idle time.
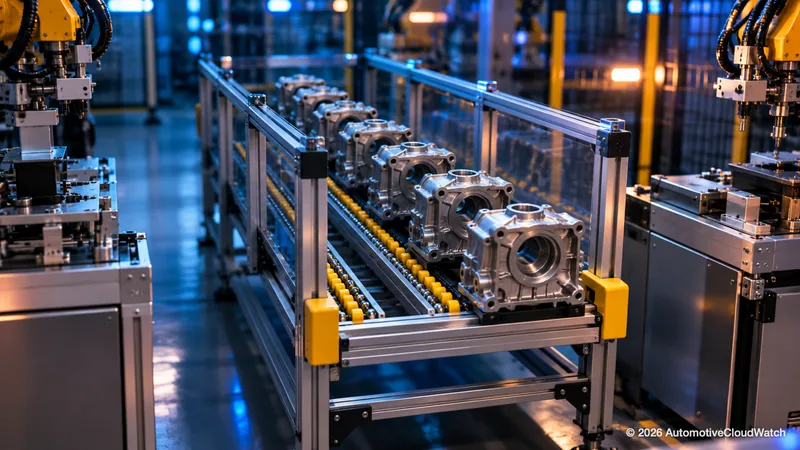 FIFO Lane Lane or rack between two processes that holds a fixed number of items in first in, first out order and stops upstream work when full.
- Fixed-Position Stop System Andon setup on moving lines where a cord pull stops the line only at the end of the work zone, giving the team leader time to fix it.
- Flow Kaizen Improvement of material and information flow across a whole value stream, usually led by managers, as opposed to station level process kaizen.
- Future State Map Value stream map showing how a process should work after improvements, usually 6 to 12 months out, which becomes the improvement plan.
- Gemba Japanese for the real place, meaning wherever value is created, usually the shop floor, where lean managers go to see problems firsthand.
- Gemba Walk Planned visit by leaders to where work happens to observe, ask questions and support problem solving, rather than to blame or give orders.
- Genchi Genbutsu Toyota Way principle of going to see the actual thing at the actual place so decisions rest on direct observation, not secondhand data.
- Group Leader GL Toyota style supervisor responsible for several team leaders and their teams, owning the section's safety, quality, output and cost.
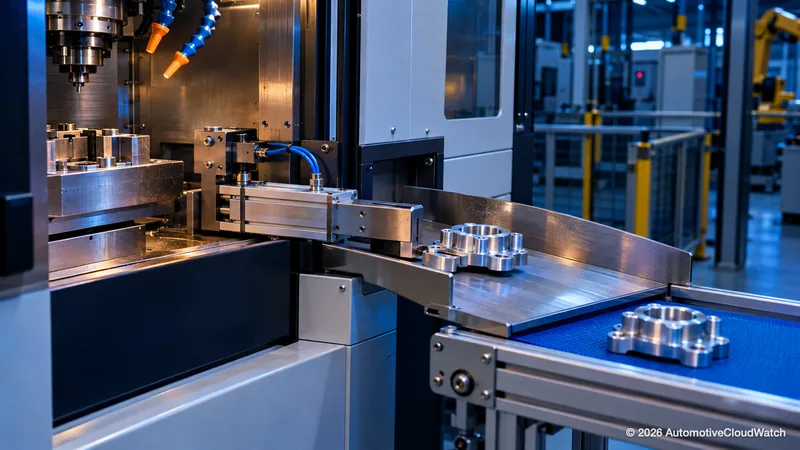 Hanedashi Device that automatically ejects a finished part from a machine at the end of its cycle, so the operator only loads the next part.
- Hansei Japanese for self reflection, the habit of honestly owning mistakes and identifying what to do better, even after a successful project.
- Heijunka Leveling production volume and product mix evenly over time so upstream processes and suppliers see steady, predictable demand.
- Heijunka Box Scheduling board with slots per product and time interval into which kanban are placed to release work in a smooth, leveled order.
- Ho-Ren-So Japanese workplace rule of report, inform and consult, meaning staff keep bosses and colleagues updated and seek advice early.
- Hoshin Kanri Strategy method that turns a company's few most important goals into aligned plans at every level, from executives to the shop floor.
- Improvement Kata Four step routine of Toyota Kata that sets a direction, studies the current condition, sets the next target condition and experiments toward it.
- Internal Setup Changeover work that can only be done while the machine is stopped, so every minute of it is lost production time.
- Jidoka Toyota Production System pillar in which machines and people detect a problem and stop at once so a defect is never passed on.
- Jishuken Hands on Toyota workshop in which managers or experts solve real shop floor problems themselves, often with suppliers, to build skill.
- Job Breakdown Sheet JBS Training worksheet listing a job's important steps, the key points in each and the reasons, prepared before teaching the job.
- Job Instruction JI Training Within Industry method that teaches supervisors to train a job in four steps, prepare, present, try out and follow up.
- Job Methods JM Training Within Industry method that teaches supervisors to improve a job by questioning each detail to eliminate, combine, rearrange or simplify.
- Job Relations JR Training Within Industry method that teaches supervisors a four step way to handle people problems and treat workers as individuals.
- Just-in-Time JIT Toyota Production System pillar of making and delivering only what is needed, when it is needed, in the amount needed.
- Kaikaku Japanese for radical reform, a breakthrough change such as relaying out a whole plant, complementing small step kaizen.
- Kaizen Japanese for change for the better, meaning continuous, small, low cost improvement by everyone as a daily habit.
- Kaizen Burst Starburst symbol on a value stream map marking a specific improvement needed to reach the future state.
- Kaizen Event Focused workshop of about three to five days in which a cross functional team redesigns one process on the shop floor and changes it at once.
- Kaizen Promotion Office KPO Small central team of full time improvement specialists who coach managers, run kaizen events and track a lean transformation.
- Kamishibai Audit system using a board of cards, each a check to perform, that leaders draw, verify and flip to green or red for all to see.
- Kanban Japanese for signboard, a card or signal that authorizes making or moving a set quantity of parts, linking processes in a pull system.
- Karakuri Kaizen Low cost improvement using simple mechanical devices driven by gravity, springs, levers and cams instead of motors and controls.
- Lead Time Total time from request to delivery, such as from order to shipment, most of which parts usually spend waiting in queues.
- Leader Standard Work Defined routines supervisors and managers follow at set times, such as floor walks, team meetings and standard checks, to sustain gains.
- Lean Enterprise Institute LEI Nonprofit founded by James Womack in 1997 that publishes lean books, workbooks and training, including Learning to See and the Lean Lexicon.
- Lean Manufacturing Production approach derived from the Toyota Production System that delivers customer value while removing waste through flow, pull and improvement.
- Lean Product and Process Development LPPD Lean approach to designing products and their production processes, using a chief engineer, set based design and visual obeya planning.
- Lean Thinking Five principles of value, value stream, flow, pull and perfection that turned the Toyota Production System into a general management approach.
- Line Balancing Dividing line work among stations or operators so each carries about the same load, close to but not above takt time.
- Mixed-Model Production Building different product versions on one line in a mixed sequence instead of large batches, matching output to the actual order mix.
- Mizusumashi Material handler who runs a fixed timed route delivering parts to the line and collecting kanban and empties so operators stay at their stations.
- Monozukuri Japanese for the art of making things, a word expressing pride in craftsmanship, deep process knowledge and constant refinement.
- Muda Japanese for waste, meaning any activity that uses time, money or effort without adding value the customer will pay for.
- Multi-Process Handling Staffing in which one operator runs several different processes in sequence while carrying a part through a cell.
- Mura Japanese for unevenness, meaning swings in workload, volume or mix that overload people and machines at some times and idle them at others.
- Muri Japanese for overburden, meaning pushing people or equipment beyond what they can reasonably handle, leading to injury, breakdowns and defects.
- Nemawashi Practice of quietly talking a proposal through with everyone affected before a formal decision, so support is built in advance.
- Non-Value-Added Activity NVA Any step that uses time or resources without changing the product in a way the customer pays for, such as moving, waiting or inspecting.
- Obeya Japanese for big room, a dedicated project room whose walls show schedules, metrics, problems and designs so a team sees status at once.
- Ohno Circle Teaching exercise in which a manager stands inside a circle drawn on the floor and watches a process until they see the waste for themselves.
- One-Touch Exchange of Die OTED Extension of SMED that aims to finish a changeover in under one minute, ideally with a single action such as one turn or push.
- Pacemaker Process Single point in a value stream that receives the customer schedule and sets the pace for all upstream and downstream processes.
- Pitch Time needed to make one standard container of product, takt time times pack quantity, used as the interval for releasing work and checking progress.
- Plan-Do-Check-Act PDCA Four step improvement cycle of plan a change, try it small, check results against expectations, and adopt or adjust it.
- Point of Use Storage POUS Keeping parts, tools and materials right where they are used instead of a central storeroom, cutting walking and searching.
- Poka-Yoke Japanese for mistake proofing, a device or design feature that makes an error impossible or obvious the moment it happens.
- Practical Problem Solving PPS Toyota's structured method that narrows a vague problem to its point of cause by going to see, then uses why analysis to find the root cause.
- Process Capacity Sheet Standard form recording manual, machine and tool change time for each machine to find the process's maximum output and its bottleneck.
- Product Family Matrix Table of products against process steps that groups products sharing most steps into families for value stream mapping.
- Production Kanban Kanban card or signal that tells a process to make a specific quantity of a specific part after the downstream process uses it.
- Production Preparation Process 3P Method in which a cross functional team sketches and mocks up several alternative production processes before buying equipment.
- Pull System Production control in which nothing is made until the next process or customer uses something and signals a need.
- Push System Production control in which work is released by forecast or schedule whether or not the next process is ready, which tends to build inventory.
- Red Tag Tag placed during the 5S sort step on any item of doubtful need, which is moved to a holding area and later kept, moved or discarded.
- Respect for People Toyota Way pillar holding that employees should be developed, trusted and involved in solving problems rather than treated as labor.
- Sensei Japanese for teacher, an experienced lean practitioner who coaches others, often by asking questions on the shop floor instead of giving answers.
- Sequential Pull System Pull system in which processes build items one by one in the exact order of a schedule sent to the line start, rather than refilling a store.
- Set-Based Concurrent Engineering SBCE Development approach that keeps several design options open and narrows them as evidence grows instead of committing early to one design.
- Seven Wastes Taiichi Ohno's seven kinds of production waste, overproduction, waiting, transport, overprocessing, inventory, motion and defects.
- Shadow Board Tool board marked with the outline of each tool in its place, so a missing tool is noticed at a glance.
- Shigeo Shingo Japanese industrial engineer (1909 to 1990) who worked with Toyota and developed the SMED quick changeover and poka yoke methods.
- Shingo Prize Operational excellence award named after Shigeo Shingo and run by the Shingo Institute at Utah State University since 1988.
- Shojinka Flexible staffing that changes the number of operators on a line to match demand while keeping productivity high.
- Shoninka Reducing the number of operators a process needs through improvement, with freed people redeployed rather than laid off.
- Signal Kanban Kanban for batch processes such as stamping, placed at a set point in a container stack so reaching it triggers a full batch.
- Single-Minute Exchange of Die SMED Shigeo Shingo's method for cutting machine changeover time to under ten minutes, enabling smaller batches, less inventory and shorter lead time.
- Skills Matrix Grid of team members against tasks showing each person's skill level, used to plan job cover and training.
- Spaghetti Diagram Overhead drawing of a work area tracing the path of a person, part or document, revealing wasted walking and transport.
- Standard Work Written current best way to do a job, with step order, timing and parts on hand, forming the basis for training and improvement.
- Standard Work in Process SWIP Smallest number of parts that must be inside a process, including in machines, for an operator to follow standard work without waiting.
- Standardize-Do-Check-Act SDCA Cycle for holding a process at its current standard, follow it, check results and correct slippage, in contrast to PDCA for improving it.
- Standardized Work Chart One page overhead drawing of a workstation showing the operator's path, work order, standard stock and checkpoints, posted for training and audits.
- Standardized Work Combination Table Chart plotting one operator's manual, walking and machine automatic times against takt to show whether the work fits and where waits occur.
- Start-of-Shift Meeting Short stand up meeting at each shift start where a team reviews safety, results, quality alerts, staffing and the day's plan at its board.
- Stop-Call-Wait Operator rule to stop work, call for help, usually with the andon, and wait for the team leader instead of fixing it alone or passing it on.
- Supermarket Controlled store between two processes holding a fixed amount of each part, refilled by the upstream process only as parts are taken.
- Supplier Kanban Kanban between a plant and an outside supplier authorizing delivery of a set quantity on a set schedule based on actual use.
- Taiichi Ohno Toyota engineer and executive (1912 to 1990) regarded as the chief architect of the Toyota Production System and the kanban system.
- Takt Time Pace at which products must be finished to meet customer demand, available working time divided by units required.
- Takumi Japanese for master craftsman, a title for highly skilled veteran workers at firms such as Toyota and Nissan who train others and check processes.
- Target Condition Toyota Kata description of how a process should operate and what results it should achieve by a set future date.
- Team Leader TL Hourly worker in a Toyota style plant who leads about four to eight operators, answers andon calls, covers absences and leads daily improvement.
- Teian Japanese word for suggestion, used for employee systems in which frontline workers submit and carry out many small improvement ideas.
- Three Actuals Japanese principle of sangen shugi, go to the actual place, see the actual thing and understand the actual facts before deciding.
- Toyota Business Practices TBP Toyota's standard eight step problem solving method, from clarifying the problem to standardizing successful countermeasures.
- Toyota Kata Management approach that builds problem solving habits through short repeated routines, described by Mike Rother in his 2009 book.
- Toyota Production System TPS Toyota's manufacturing system for making exactly what customers need with minimal waste, built on just in time and jidoka.
- Toyota Way Toyota's formal management philosophy, built on the two pillars of continuous improvement and respect for people.
- TPS House Diagram of a house showing how the Toyota Production System fits together, with pillars of just in time and jidoka on a base of stability.
- Training Within Industry TWI World War Two US government program that trained supervisors in job instruction, job methods and job relations, later adopted in Japan.
- Two-Bin System Stocking method with two containers per part at the point of use, where the empty first bin becomes the reorder signal.
- U-Shaped Cell Cell layout with machines in a U so the process start and end sit close together, cutting walking and easing staffing changes.
- Value Stream All the steps, value adding or not, needed to take a product from raw material or concept to the customer.
- Value Stream Mapping VSM Method of drawing on one page how material and information flow through every step from supplier to customer, then designing a better flow.
- Value-Added Activity Any step that changes the product in a way the customer will pay for and is done right the first time, such as machining or assembly.
- Visual Management Designing a workplace so anyone can see at a glance what is normal and whether something is wrong, using boards, markings and signals.
- Waste Walk Walk through a work area specifically to spot and record waste such as waiting, extra motion, transport and excess inventory.
- Withdrawal Kanban Kanban card authorizing a material handler to move a set quantity of parts from a supplying process or store to the process using them.
- Work Element Smallest piece of work that can be moved to another operator or station, timed individually for line balancing.
- World Class Manufacturing WCM Structured improvement system developed with Hajime Yamashina that combines TPM, TQC and JIT into audited pillars, used across Stellantis.
- X-Matrix One page hoshin kanri chart linking breakthrough goals, annual goals, top projects, metrics and owners through grids around a central X.
- Yamazumi Chart Stacked bar chart of each operator's or station's work against a takt time line, showing which are overloaded and which have spare time.
- Yokoten Japanese for horizontal deployment, spreading a proven improvement or lesson across other lines, plants or departments to be adapted.
Full entry for members
Every term has a full entry for members: the plain-words definition, the practitioner note and the typed links between terms.
ACW Manufacturing Glossary, edition 2026.11.1. The headword and one line are open to everyone.